


Seamless Hydraulic Cylinder Tube (EN 10305-1 E355 / ASTM A519 1020)
Cold drawn seamless tube for hydraulic cylinder barrels, OD 50-325 mm, wall 5-40 mm, E355 / E235 / A519 1020 / 1045, wall eccentricity within 5 percent, stress relieved after drawing, UT and hydro tested, 3.1 MTC per heat.
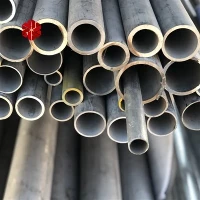
Barrel stock for hydraulic cylinders, supplied as cold drawn seamless tube. Cylinder shops buy it, bore and hone the inside, weld a gland and a base, and put a piston in it. The sizes that move are 50 to 325 mm outside diameter, 5 to 40 mm wall, 40 to 300 mm inside diameter, in E355, E235, A519 1020 and 1045.
Our route: pierce, roll, cold draw in two passes, stress relieve at 540 °C, straighten on a six-roll machine, inspect. The pierced hollow is ours, so the heat number stamped on the tube is the heat number printed on the certificate.
Wall eccentricity is where cylinder tube gets rejected. Mandrel sits 0.1 to 0.2 mm off centre, the wall comes out 3 to 5 mm heavy on one side across 6 m. OD check passes. ID check passes. Then the shop bores it, cuts the heavy side first, and finishes under minimum wall on the light side. We hold 5 percent eccentricity on cylinder stock and print it. Standard stock is 10 percent and costs less per tonne.
Specifications
| Item | Range |
|---|---|
| Standard | EN 10305-1, ASTM A519, GB/T 3639 |
| Grades | E235, E355, E355 +SR; A519 1020, 1045; ST52 |
| Outside diameter | 50 – 325 mm |
| Wall thickness | 5 – 40 mm |
| Inside diameter | 40 – 300 mm |
| ID tolerance | H10 as drawn; H9 only on honed stock, not on drawn stock |
| Wall eccentricity | ≤ 5 percent for cylinder stock, 10 percent standard |
| Straightness | 1 mm per metre, 4 mm total on 6 m |
| Length | 5.8 m and 6 m; cut 3 – 7 m to order |
| Condition | Cold drawn, stress relieved, pickled or bright annealed |
| Ends | Square cut, beveled, plastic caps |
| Testing | Hydrostatic; ultrasonic per EN 10216-2 class; eddy current on request |
| OD tolerance | ±0.5 mm to 120 mm, ±0.8 mm above |
| Documents | EN 10204 3.1 per heat, 3.2 by third party |
Order the bore under nominal if you hone in house
Most cylinder shops hone their own barrels and still order the finished inside diameter from the drawing. That leaves the hone the full drawing tolerance plus the draw marks, 0.1 to 0.2 mm a side, and one extra pass per tube. Order 0.3 to 0.4 mm under nominal instead. The hone cleans up in one pass and the wall stays where the drawing put it.
If you want the bore finished, say it at enquiry. Honing is a separate operation at a separate price and we do not run it here. A drawn tube sold as honed is a claim we are not willing to make, and the Ra number is the first thing that exposes it.

Stress relief, 540 degrees, two hours
Drawing leaves stress in the wall and it does not show up in a dimensional check. It shows up after machining and welding, when the barrel moves. We soak at 540 °C for two hours, cool in still air, straighten, then re-check straightness.
One customer in Izmir machined a 200 mm barrel, welded the port block, and found the last 400 mm of bore 0.15 mm off line once the weld cooled. Unrelieved tube. The welder spent a month defending himself.
Order of operations matters. Relieve first. Straighten second. Machine third. A shop that machines drawn tube straight off the truck is rolling dice on the weld.

Test scope
Tensile and chemical on every heat. Ultrasonic along the wall for lamination and centreline defects on barrels above 160 bar working pressure. Hydro at 1.5 times the design pressure you give us. If you do not give us a pressure, we test to our standard and print the figure on the certificate instead of leaving the column blank.
Hardness is read on the sample ring rather than the tube end. Cutting work hardens the end by 10 to 15 HB and a reading taken there can fail a tube that meets the spec. Wall thickness gets gauged at four points on every piece of cylinder stock, sampled on standard stock. Straightness is checked after straightening, on the table, never before. Draw marks on the OD are allowed to 0.05 mm. The ID is the surface the hone sees, and that is where we spend the finishing time.

Weight, and what fits in a box
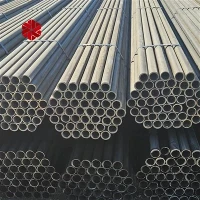
A 273 x 25 barrel runs about 153 kg per metre. Six metre pieces are close to a tonne each, so a 20 ft reaches its 25 t limit at around 160 pieces, well before the floor is full. Tell me the size and quantity and I will load-plan it before you book freight. Hex bundles, steel strap, caps on both ends, one tag per bundle with heat, size and piece count.
Request a Quote
Send OD, wall or ID, grade, length, and whether you hone in house. If the cylinder holds pressure, add the working pressure and the bore finish you need. Reply within 12 hours with price, tonnage per container and the test papers we can attach to the offer.


Send Inquiry
